
NEWS
Uneven Brine Distribution: Process Checks for a Saline Injection Machine
Uneven brine distribution deserves immediate attention because it can create several problems at once: inconsistent flavor, variable cooked yield, localized texture defects, and uncertainty around process control. A product may still meet an average pickup target while individual portions receive too little or too much brine. For quality and food safety teams, the question is therefore not simply whether the Saline Injection Machine is operating, but whether it is delivering the intended amount uniformly across the product.
The most useful response is a structured process check that starts with the product pattern and moves upstream through needles, brine condition, pressure, conveying, and sanitation. Changing pump settings first can hide the underlying cause and create a new imbalance elsewhere.
Start by defining what “uneven” looks like
Before opening the machine, separate a true injection-distribution problem from variation caused later in the process. Compare pieces from different positions across the conveyor width, as well as the leading and trailing portions of the same batch. Record individual weights before and after injection, then compare pickup by position rather than relying only on the batch average.
Several patterns can point the investigation in different directions:
- One side of the belt shows lower pickup: suspect blocked needles, uneven manifold flow, belt tracking, or an incorrectly levelled injector head.
- Alternating high and low pickup across product rows: inspect needle groups, valve timing, and product support during the injection stroke.
- Pickup falls over the course of a run: look at brine temperature, settling solids, filter loading, foaming, or a pressure change as the reservoir level drops.
- Exterior leakage increases while average pickup remains stable: the product may be over-pressurized locally, the needles may be damaged, or the brine formulation may not be passing cleanly through the system.
A visual examination of sliced product can support this work, but it should not replace weight-based checks. Surface appearance can be misleading, particularly where product shape, fat cover, or muscle structure affects brine retention.
Inspect needle condition and alignment before adjusting pressure
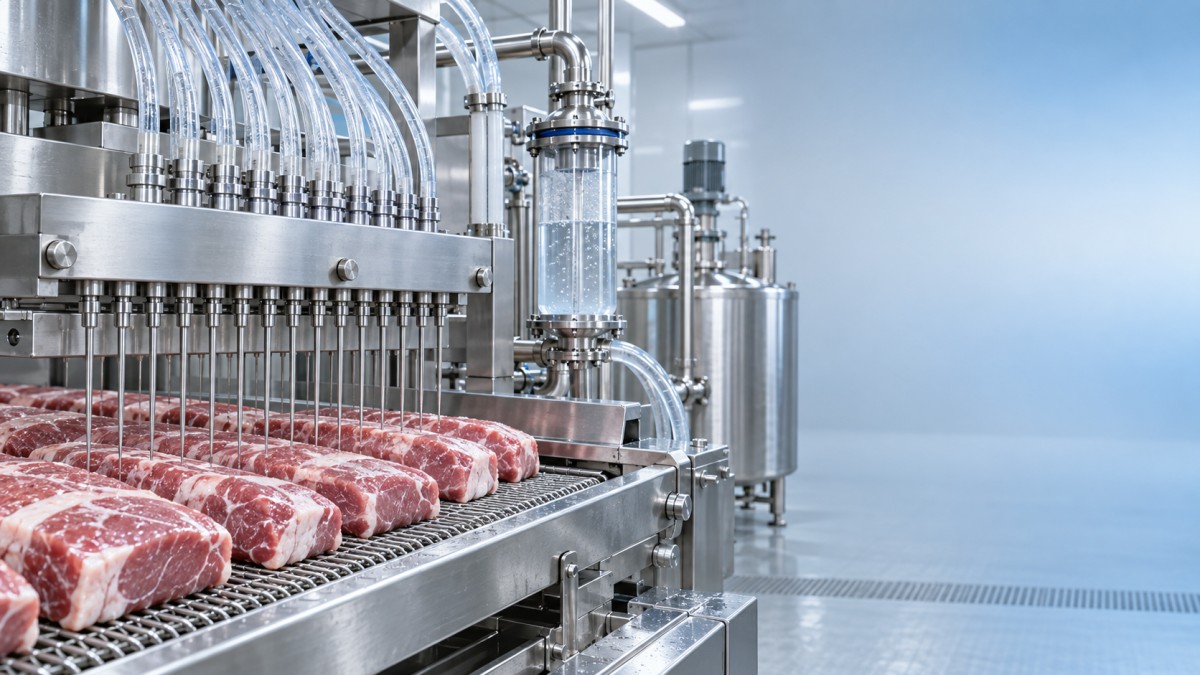
Needle problems are among the most direct causes of uneven distribution. A partially blocked needle may still pass enough liquid to avoid an obvious alarm while delivering substantially less than adjacent needles. Bent, blunted, worn, or incorrectly seated needles can also change penetration depth and leave some areas under-injected.
Inspect needles in a controlled shutdown and check for deposits inside the bore, residue around outlets, damaged tips, and inconsistent projection from the needle bridge. Cleaning should confirm that each flow path is open, not merely that the exterior looks clean. If the equipment design allows a flow or spray-pattern verification, compare all needle positions rather than testing only a few accessible points.
Alignment matters as much as cleanliness. The product must be supported at a consistent height when the needle bridge descends. A tilted conveyor, worn support belt, product pile-up, or poor spacing can make identical needle settings behave differently across the belt. This is particularly important for variable-thickness cuts, where an injection pattern that works on a uniform muscle may cause leakage or shallow injection on uneven pieces.
Check the brine as a process fluid, not just a recipe
A correct formulation can still perform poorly if it is not physically stable in circulation. Undissolved ingredients, protein particles, spice fragments, fat, and small pieces of product tissue can restrict filters and needle channels. Separation or settling changes the concentration reaching the product, especially when the tank is not mixed adequately or the line runs for an extended period.
During an investigation, verify that the brine is fully prepared and held under the intended conditions before it enters the injector. Review filtration condition, mixing performance, tank agitation, return flow, and foam formation. Excess foam can make pump delivery less consistent because entrained air changes how the system fills and discharges.
Temperature should also be treated as a control point. A change in temperature can alter viscosity and the behavior of ingredients in suspension. The appropriate operating range depends on the formulation and the site process, but quality teams should define an internal range and investigate movement outside it rather than treating every pressure deviation as a mechanical fault.
Match pump pressure, conveyor speed, and product geometry
Increasing pressure is a common reaction to low pickup, yet it is rarely a complete fix. Higher pressure may force brine through a restricted system or into a product with poor support, producing localized flooding and visible purge rather than better internal distribution. Conversely, low pressure may leave central areas under-injected even when the surface appears adequately treated.
Assess pressure together with conveyor speed, stroke frequency, needle density, and product thickness. A faster belt reduces exposure to the injection pattern; a slower belt can increase pickup but may also increase damage and leakage if the rest of the settings are unchanged. The objective is repeatable penetration and retained distribution for the specific product, not the highest possible injection rate.
For this reason, setting changes should be made one at a time and evaluated with representative samples from across the belt. Document the setting, product specification, brine condition, pickup variation, and any leakage observed. A record that links these factors is more useful than a single target pressure on an operator sheet.
Do not overlook sanitation-related flow restrictions
Distribution issues can emerge after cleaning when residues remain in needle assemblies, manifolds, hoses, filters, or return lines. Incomplete rinsing can also leave cleaning chemical residues that affect brine behavior or create a food safety concern. A sanitation release should therefore include confirmation that the machine is fully drained, rinsed as required by the site procedure, reassembled correctly, and returned to service without damaged seals or loose connections.
Hygienic design supports this work, but it does not remove the need for verification. Stainless construction is valued in meat processing because it supports cleaning and durability, while removable or accessible components make inspection more realistic during a production schedule. The practical question is whether the site can consistently inspect the parts that influence product contact and liquid flow.
Where brine injection is followed by further portioning, filling, or sausage production, downstream controls should protect the uniformity achieved upstream. For example, a clipping step with stable, adjustable closure settings can help prevent leakage from filled sausage products; equipment such as a Sausage Clipper may be relevant where quantitative filling and casing closure are part of the same controlled production flow. It does not correct uneven injection, but it can prevent a separate packaging-stage loss from being mistaken for poor brine retention.
A practical escalation sequence
When uneven distribution is identified, avoid returning the line to normal solely because the average pickup is acceptable. First confirm the affected product positions and lot conditions. Then inspect filters, brine circulation, needle flow paths, and mechanical alignment before changing process settings. After correction, run a defined verification sample across the belt width and through enough production time to show that the result remains stable.
If the issue repeatedly returns, treat it as a control-system problem rather than an isolated operator adjustment. The maintenance interval for filters and needles, the brine preparation method, the sanitation inspection points, and the acceptance criteria for pickup variation may need to be tightened. Consistent brine distribution comes from keeping those controls connected, so that one weak point does not turn a stable injection program into a variable product outcome.
Product Center
Leave a message online